Conveyor Control Wiring 101: How Accurate Schematic Drawings Prevent Costly Downtime
CONTROL WIRING REQUIREMENTS
Conveyor control wiring connects power equipment, sensors, safety devices, programmable logic controllers, variable frequency drives, human-machine interfaces, and field devices into one operating system.
Accurate schematic drawings define:
- Component locations
- Wire numbers
- Terminal assignments
- Device tags
- Motor connections
- PLC input and output points
- VFD control circuits
- Safety circuits
- Control voltage levels
- Field connection points
- Panel wiring requirements
- Revision status
When the drawings match the physical panel and installed field wiring, technicians can isolate faults without tracing every conductor manually. When drawings are incomplete or outdated, troubleshooting becomes dependent on guesswork, undocumented modifications, and extended production interruptions.
Conveying Controls L.L.C. provides system concept development, procurement support, FLA calculations, panel control wiring, machine control wiring, conveyor control wiring, PLC integration, HMI integration, and comprehensive schematic drawings.
With more than 35 years in the field, the company supports the complete control system process from initial specification through installation and service.
SCHEMATIC DRAWING STRUCTURE
A usable conveyor control drawing set requires a consistent structure. Each page should provide one defined function and connect clearly to the pages before and after it.
A complete drawing package commonly includes:
COVER PAGE
- Project name
- Customer name
- System identification
- Applicable voltage levels
- Drawing index
- Revision history
- Engineering approval information
LEGEND AND NOTES
- Electrical symbols
- Wire color conventions
- Device tag format
- Terminal identification rules
- Abbreviations
- Safety notes
- Customer-specific requirements
POWER DISTRIBUTION
- Main disconnect
- Circuit breakers
- Fuses
- Transformers
- Power supplies
- Grounding connections
- Motor branch circuits
MOTOR CONTROL
- Contactors
- Overloads
- VFDs
- Motor starters
- Brake circuits
- Run permissives
- Fault contacts
CONTROL CIRCUITS
- Start and stop devices
- Selector switches
- Control relays
- Pilot lights
- Reset circuits
- Interlocks
PLC AND HMI CONNECTIONS
- Input assignments
- Output assignments
- Analog signals
- Communication connections
- HMI devices
- Network hardware
FIELD TERMINATIONS
- Terminal block layouts
- Cable schedules
- Sensor connections
- Photo-eye connections
- Motor connections
- External control connections
PANEL LAYOUT
- Component locations
- Wire duct
- DIN rail
- Terminal blocks
- Cooling equipment
- Nameplate locations
- Enclosure dimensions
Each device should use one unique identifier throughout the drawings, panel labels, wire markers, PLC program, and maintenance documentation.
PANEL WIRING ACCURACY
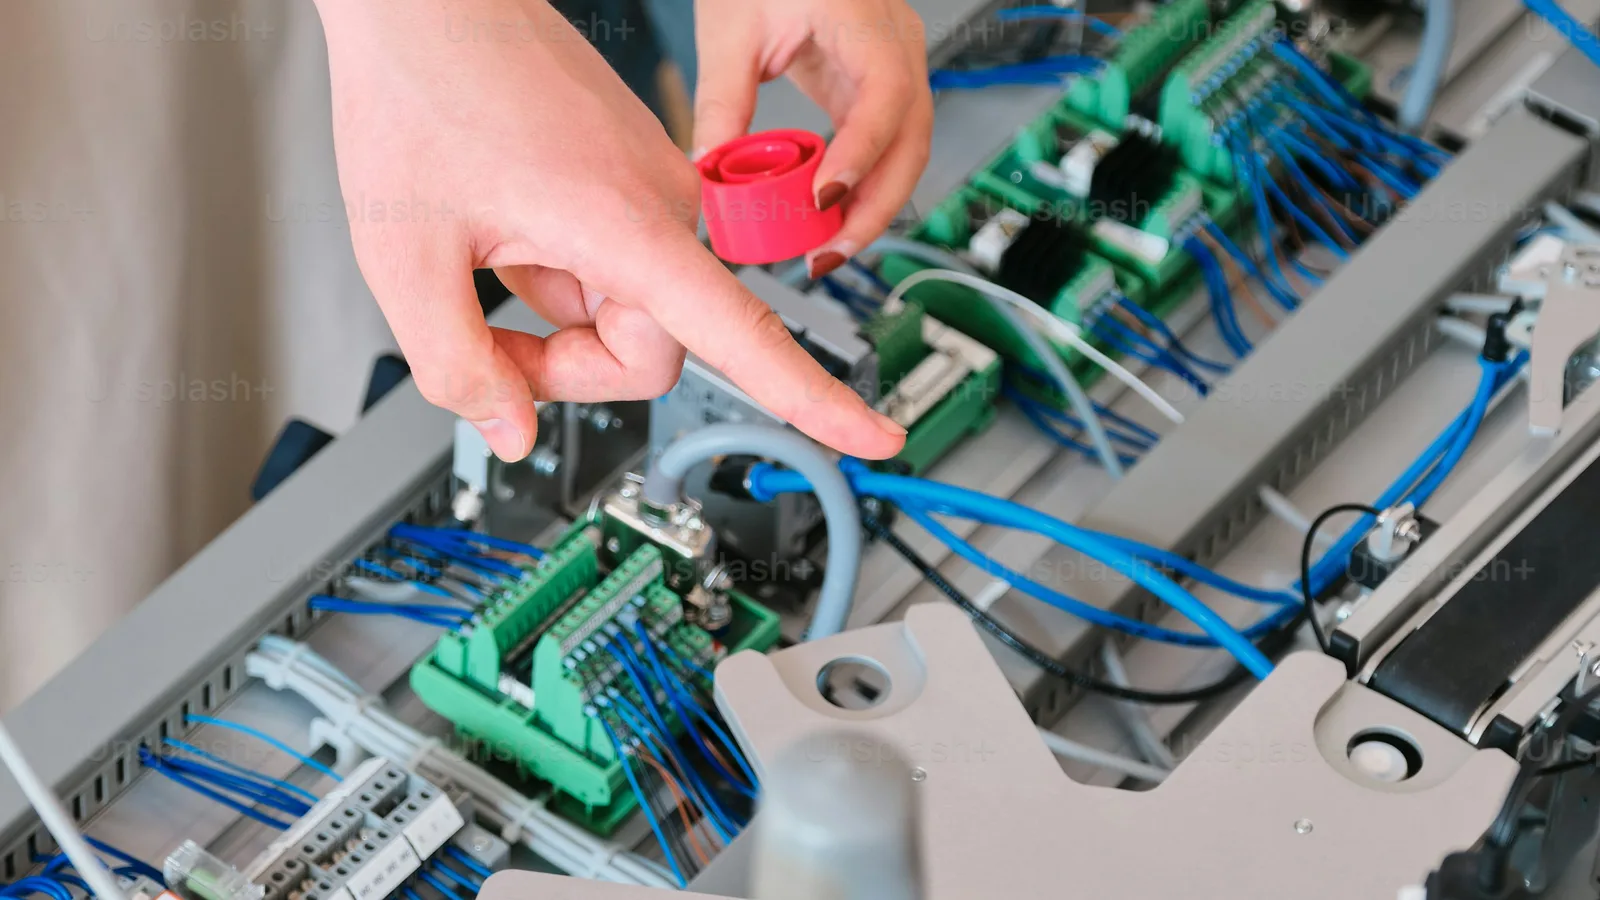
Panel wiring should follow the schematic from the first conductor to the final terminal. The following controls support consistent construction:
- Match each wire number to the drawing.
- Match each terminal number to the terminal schedule.
- Use wire markers at both conductor ends.
- Use ferrules where specified for stranded conductors.
- Maintain clear separation between power and control wiring.
- Route conductors through defined horizontal and vertical paths.
- Leave service slack at terminations.
- Maintain bend radius requirements.
- Reserve space for future additions.
- Use terminal blocks for structured field connections.
- Verify torque values according to component specifications.
- Document every field modification.
Power wiring, motor wiring, VFD output wiring, analog signals, communication cables, and low-voltage control wiring require physical planning. Separate wire duct or defined routing zones reduce interference and simplify service access.
High-energy circuits should remain separated from sensitive control and communication wiring. Where conductors must cross, routing at right angles can reduce coupling. Shielded cable requirements should follow the equipment manufacturer’s instructions and project specifications.
CONVEYOR-SPECIFIC CIRCUITS
Conveyor systems contain multiple control points distributed across a machine or production line. The drawings must identify how each device affects operation.
Typical conveyor control points include:
- Motor run commands
- VFD enable signals
- VFD fault outputs
- Motor overload contacts
- Pull-cord emergency stops
- Guard switches
- Photo-eyes
- Proximity sensors
- Jam detection sensors
- Zero-speed switches
- Belt alignment switches
- Start permissives
- Downstream permissives
- Upstream interlocks
- Manual and automatic selector switches
- Local and remote control stations
A conveyor drawing should show the relationship between each device and the control sequence. For example, a photo-eye may provide a PLC input, while the PLC output controls a VFD run command. A downstream conveyor may need to prove operation before an upstream conveyor starts. A jam sensor may remove a run permissive and initiate an alarm.
These relationships require clear wire numbers, device tags, terminal references, and PLC address assignments.
Safety circuits require separate documentation and verification. Emergency stops, guard switches, safety relays, and other protective devices should not be treated as ordinary sensor inputs. The drawing should identify the safety circuit, reset requirements, monitored contacts, and affected equipment.
PLC, HMI, AND VFD DOCUMENTATION
Industrial control systems depend on alignment between electrical drawings and software configuration.
The documentation should identify:
- PLC rack and slot numbers
- Input and output addresses
- Terminal numbers
- Field device descriptions
- VFD parameter references
- HMI tag names
- Network addresses
- Alarm descriptions
- Motor identification
- Control mode selection
- Fault reset functions
A mismatch between the schematic and PLC program can create symptoms that appear to be software faults but originate in panel wiring, terminal assignments, incorrect sensor polarity, or missing control voltage.
VFD circuits require separate identification for:
- Incoming line power
- Motor output power
- Start and stop commands
- Speed references
- Enable signals
- Run status
- Fault status
- Emergency stop interface
- Braking or regeneration equipment
- Shielding and grounding
The drawing package should distinguish between power wiring and low-voltage control wiring. This separation supports safer testing and faster fault isolation.
FLA CALCULATIONS AND COMPONENT SELECTION
Full-load amperage calculations support the selection of conductors, overload protection, disconnects, fuses, breakers, contactors, VFDs, and other control system components.
The documented calculation process should consider:
- Motor horsepower
- Motor voltage
- Phase configuration
- Full-load amperage
- Service factor
- Motor quantity
- Simultaneous operation
- Ambient conditions
- Conductor length
- Voltage drop
- Starting requirements
- VFD application
- Protective device ratings
FLA calculations should correspond with the motor schedule, panel layout, schematic drawings, and procurement list. Inconsistent information can result in incorrect component selection, delayed procurement, panel modifications, or field rework.
Conveying Controls supports FLA calculations and procurement specifications as part of the control system design process. Additional capabilities are outlined on the Conveying Controls services page.
COMMISSIONING AND VERIFICATION
Accurate drawings provide the basis for point-to-point testing before energization and commissioning.
A verification process should include:
- Confirming device tags
- Checking wire numbers
- Verifying terminal assignments
- Inspecting conductor routing
- Checking protective earth continuity
- Confirming control voltage
- Verifying fuse ratings
- Checking overload settings
- Testing emergency stop circuits
- Testing interlocks
- Confirming sensor polarity
- Verifying PLC input response
- Verifying PLC output response
- Checking VFD commands and faults
- Confirming HMI indications
- Recording field changes
Testing should proceed from the drawing set. Each tested point should be marked, logged, or otherwise documented. Any change discovered during installation or commissioning should receive a drawing revision.
AS-BUILT DOCUMENTATION
As-built drawings must reflect the installed system. A drawing package that represents the original design but not the final installation creates future service risk.
Update the documentation when:
- A device changes location.
- A terminal assignment changes.
- A wire is rerouted.
- A sensor is replaced with a different model.
- A VFD is changed.
- A control voltage changes.
- A field device is added.
- A safety circuit is modified.
- A PLC input or output is reassigned.
- A panel component is substituted.
The final document set should include the latest schematic drawings, panel layout, terminal schedule, cable schedule, I/O list, equipment list, and applicable calculation records.
REDUCING DOWNTIME THROUGH DESIGN
Accurate conveyor control wiring documentation reduces downtime through defined access to system information.
The operational controls are direct:
- IDENTIFY each device with a consistent tag.
- NUMBER each conductor and terminal.
- SEPARATE power, control, and communication wiring.
- DOCUMENT PLC, HMI, and VFD interfaces.
- VERIFY every connection before startup.
- RECORD field modifications.
- UPDATE as-built drawings.
- STORE the final document package where maintenance personnel can access it.
The result is a control system that can be installed, commissioned, modified, and serviced using the same technical reference.
For conveyor projects requiring concept development, panel wiring, FLA calculations, PLC and HMI integration, or comprehensive schematic drawings, CONTACT Conveying Controls L.L.C..
© Conveying Controls L.L.C. All rights reserved.